No products in the cart.


Newsletter
[contact-form-7 id=”4235″ title=”Contact form 1″]

Part 3 closed on an uncomfortable admission: when guillochage à main is executed perfectly, it is difficult to separate from a well executed CNC guillochage. That is not a failure of the diagnostic method. It is the diagnostic method working correctly and arriving at the honest answer. Where a machine can match the hand, it does, and no amount of looking will change it.
Which is why the techniques in this final technical instalment are worth reading in pairs of questions rather than one.
Part 3 dealt with techniques that cut into metal — gravure and guillochage. The operations here work differently. One displaces metal to raise a relief. One removes it to open the movement up. Three texture a surface by abrasion. Two add a metal that was not there before, one mechanically and one by electrolysis.
The first question is whether the work was done by hand or by machine.
The second, which watch aficionados ask less often and which matters more, is whether hand work is done well or merely done. A poorly executed hand finish is not superior to a competent machine finish. It is technically worse, it is more expensive, but still delivers the hand-made look.
Patek Philippe Grande Sonnerie Turbillon ©ourtesy Patek Philippe – perfect Cotes de Geneve, Perlage, Anglage, satin finished levers, cerclage, hand-mirror-polished screws


CHISELAGE – Courtesy C.Sermier & G.Papi
Ciselage is the opposite of intaglio engraving. Where engraving removes material to create a recessed design, chasing pushes the material to create an embossed design. The metal is displaced — struck with a hammer and a small bevelled steel tool called a ciselet, forcing the surrounding metal to rise and form the relief motif. The work is finished by matting — dulling the surface around the motif to even it out.
The industrial alternative is press stamping or die striking: the component is struck — coined — under mechanical pressure and the design is formed instantaneously. The result is clean and burr-free, consistent across any number of identical pieces, and entirely without individual character. The diagnostic difference from hand chasing is readable in the relief geometry: hand-chased motifs show slight variation in height and edge definition that die-struck work does not — the tool marks of the ciselet, visible under magnification, are the signature of the hand.
Establishing that it is hand work settles very little, because chasing punishes the inexpert more visibly than almost any other technique. Displaced metal work-hardens, and a chaser who has struck the same area too often produces a dull orange-peel texture across the relief, or in the worst cases a hairline crack. Look for even relief height across the whole motif, and for edges that stay crisp where the design turns: good chasing holds definition through a curve, indifferent chasing lets it soften into a mound.
The matting should be uniform, including in the tight spaces between raised elements, where a rushed job leaves the original surface showing through. The finest work goes further still and undercuts the edges of the relief slightly, so the motif casts its own shadow and stands away from the ground rather than merely rising from it.
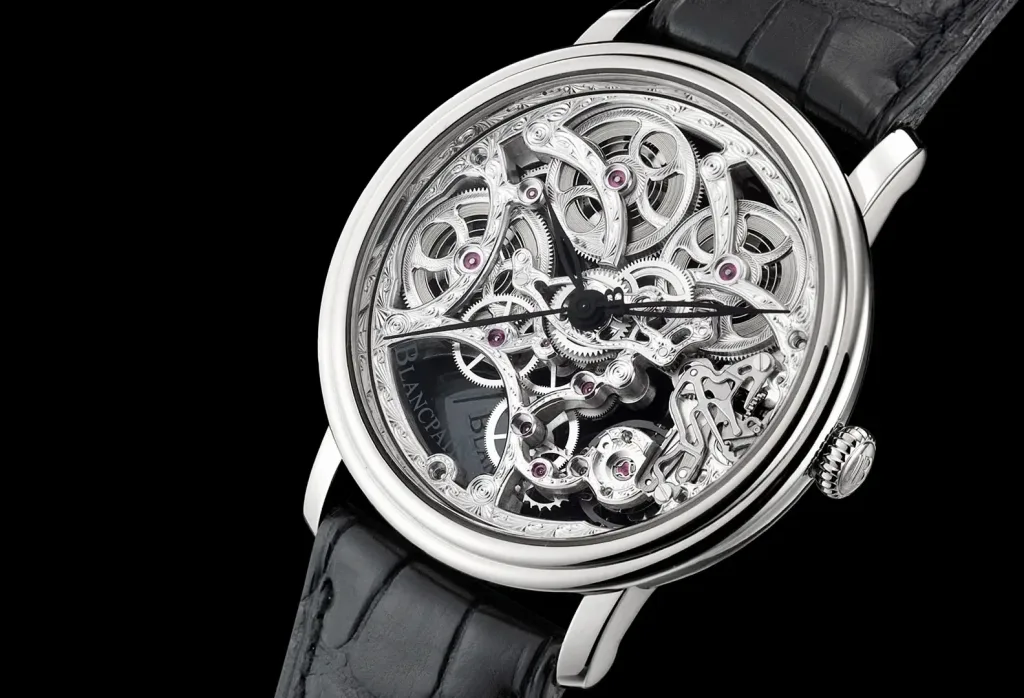
Skeletonisation creates apertures through plates and bridges to reveal the mechanism, without touching the parts that keep it running: jewel seats, screw points, the sectors where the gear train works. The design must be drawn before any cutting begins, because what can safely be removed is dictated by the movement`s architecture, and once made a cut cannot be undone.
GERALD GENTA SQUELLETTE Ref. 1955


The process starts with small pilot holes, through which the blade of a piercing saw is threaded. From there the cut is made perpendicular. Any bias in the blade produces aperture walls that are not parallel, which is visible under a loupe and immediately damning.
Machine or hand is the easier question, and the answer is not in the cut. CNC produces apertures of geometric perfection; hand cutting rarely matches it for outline regularity. Look at the walls instead. A properly finished skeleton has every aperture wall drawn to remove the saw marks, then satined, then anglaged around the full perimeter — with sharp internal corners at every intersection, exactly as described in Part 1. Machine work leaves the walls in a more rough condition.
Gerald Genta Ref. 2063 the quality of this Ajourage is seen by the thinness of the bridges, the hand engraved surfaces, polished walls, anglage, cerclage
The second question separates serious ateliers from the rest. Low-grade hand skeletonisation shows saw marks surviving inside the apertures, walls dressed on the visible face and ignored where the eye does not immediately fall, anglage that stops short at difficult corners or narrows where the file could not reach. High-grade work is consistent all the way round, including on aperture edges that face inward and will be seen by almost nobody.

Gerald Genta Ref. 2063

A Hand-Engraved balance cock on a Breguet Pocket Watch

An Industrial-Grade skeleton movement
The balance cock is where this began. From the seventeenth century the coq was skeletonised and engraved with animals, flowers, foliage and faces, and the coq of a verge watch has always been regarded as a small work of art in its own right — independent of the movement it regulated.

These three belong together because they share a method: an abrasive tool rotated against the component, with the orientation of the tool determining the pattern.
Soleillage décoration – Courtesy Sytem41
Soleillage (sunray on movements and rotors, sunburst on dials) produces straight lines radiating from a single point, giving the surface the look of a sun. It is achieved with a bell-shaped wheel turning counter to the piece, oriented so that every line passes through the same centre. It appears on dials, rotors and barrel covers.
Colimaçonnage (snailing) produces a spiral, and is usually found on ratchet wheels, oscillating weights, barrels and barrel covers.
Cerclage (circular brushing) is a form of smoothing that leaves fine circular lines and adds brilliance, applied by pressing a slate stick or a cabron against a rotating component. It is generally reserved for the visible faces of wheels, where it manages reflection as much as it decorates.
On the hand-or-machine question, it is a very difficult call: all three are within reach of a machine, and a competent industrial application of any of them is difficult to distinguish from a competent manual one. This is where the second question on quality does all the work.
Colimaçonnage – Courtesy System 41


Look for consistency of depth across the whole surface, not just at the centre. Abrasive tools wear, and a workshop that does not renew them produces a pattern that is crisp on the first components of a batch and progressively duller on the last. Look at the edges, where the pattern meets the perimeter of the component: it should run cleanly to the boundary without fading, smearing or throwing a burr.
Cerclage on the chrono wheels of a Lemania – Universal Geneve caliber
On soleillage, examine the convergence point, where any inconsistency in the tool’s orientation shows first. And look at whether the treatment has been applied to components the owner will never see. That is the clearest signal these three techniques give — not skill, but the consistency of a maker’s quality.
Colimaçonnage on the pallet-fork bridge of this Vacheron & Constantin caliber 435/3B


Electroplating deposits a thin layer of one metal onto another by electrolysis — nickel, gold or rhodium — at thicknesses from 0.1 microns for a flash to 20 microns for a full plating. It protects as well as decorates: brass tarnishes quickly, and gilding both preserves and improves it.
Gold shades are governed by a standardised European scale running from 1N to 5N. The point most often missed is that the standard defines each shade by chromatic coordinates rather than by chemical composition — two makers can arrive at 3N by different alloy routes provided the measured colour matches. In the metal itself, more copper reads redder and more silver reads paler.
This Looks like a 4N – Glashutte Original Calibre 58-03 – Courtesy Glashutte
| Code | Shade | Notes |
|---|---|---|
| 1N | Pale yellow | High silver content, faintly greenish cast |
| 2N | Light yellow | Pale, restrained tone |
| 3N | Yellow | The standard, and the most common in watchmaking |
| 4N | Pink | Copper-enriched; contemporary rose gold |
| 5N | Red | Deep red, highest copper content |
Compound designations such as 1N-14 or 2N-18 appear on plating specifications and case markings, combining the colour code with a karat equivalent. There is no equivalent numbered scale for white metals. White, grey and dark finishes are designated by the deposited metal itself.
“Or Noir” Coated Movement – Courtesy Laurent Ferrier


Black polishing does not belong on either table, despite the name. It deposits nothing: it is a mechanical operation on hardened steel, worked to such perfect flatness that it reflects light in a single direction, reading black when viewed perpendicular and white or grey at other angles. It belongs to a different discipline, and independent watchmaking takes it up.
Courtesy Bersenti.com
Preparation is the whole of it. The surface must be meticulously polished first, because the deposited metal covers the existing texture without altering it — concealing nothing, hiding no scratch and no tool mark.
| Metal | Appearance | Behaviour and use |
|---|---|---|
| Rhodium | Brightest white, faintly blue | Very hard, does not tarnish. Standard on high-grade movement plates and bridges. Decorative thickness typically 0.05–1.5 µm. |
| Nickel | Warmer, softer white | Tarnishes and yellows with age. Also used as an underplating beneath gold to prevent brass contaminants from migrating into the gold layer. |
| Palladium | Grey-white | Softer and greyer than rhodium. |
| Ruthenium | Gunmetal grey | Used for dark movement finishes; offers poor scratch resistance. |
| Black rhodium | Dark grey to black | Rhodium alloyed with ruthenium and other compounds; the final shade varies depending on the alloy. |
| Silver (argentage) | Warm white | Tarnishes readily. Historically used as the finish on silvered dials. |
The pieces are then suspended on copper wire, degreased, dipped in diluted sulphuric and nitric acid, and rinsed in hot water. Only then does the colouring bath follow: the components hang in a potassium cyanide solution carrying the colouring metal, an anode suspended alongside, the bath at roughly 80°C, direct current passing through. Reducing temperature and current yields a paler tone; modifying the solution shifts it further. Afterwards the pieces are ultrasound cleaned in soapy water, rinsed in hot water and then alcohol to prevent water staining, and immediately buried in sawdust — air drying invites condensation.
Which makes the diagnostic unusually simple. Plating quality is a direct readout of the finishing beneath it. Dull patches, visible scratches under the gold, blistering, pooling in recesses or at edges — none of these are plating faults. They are preparation faults, made permanent.
On a vintage movement the white finish is a quality marker as well as a decorative one. Rhodium and nickel were both in use through the mid-twentieth century, and they age very differently.
Rhodium is hard and does not tarnish: a movement plated with it in 1950 will still read crisply white today, with its côtes de Genève and perlage as sharp as the day they left the bench. Rhodium was the more expensive of the two at the time, and it was specified where the rest of the movement justified the cost.
An old Rhodium-Plated Patek Philippe movement


Nickel does not hold. It dulls, warms towards yellow, and develops dark speckling and cloudy patches — particularly around the edges of bridges and near the barrel, where handling and residual oils accelerate it.
So a seventy-year-old calibre still bright under a loupe is telling you something about how it was built.
An older NIckel-Plated movement
Also consider that an aggressive cleaning can strip plating from a movement of any grade, and a rhodium-plated bridge that has been over-cleaned will show brass at the edges rather than yellowing overall — a different failure, and one to read as service history rather than as original specification.
Rhodium-plating on an older IWC caliber

An expert eye can look at a finished surface and name the method that produced it, and that identification amounts to a quality label in itself. Two structural facts keep it that way. Some operations remain simply beyond a machine: internal corners, black polishing, the centre geometry of hand-guided work. And the volumes involved in high-grade watchmaking make the tooling investment irrational, so hand finishing remains better suited to small series than any industrial alternative.

The qualitative finish of a Longines Cal. 13.ZN

25 a finely engraved pocket-watch movement from the 1800`s

A flawless Blancpain Villeret Skeleton Watch – Courtesy of Blancpain
Beneath all of it sits the principle that governs the discipline: decoration must never compensate for a technical deficiency, and must never interfere with the mechanism. A watch, however finely finished, remains an instrument for measuring time.
Four parts have now set out the vocabulary of that discipline — what each technique is, how it is executed, and how to tell hand from machine, and good hand work from indifferent. Before applying the framework, the next post collects the terminology itself: a working glossary of the terms used across these articles and encountered daily on catalogues, auction listings and service invoices. The instalment after that puts the framework to work on the independent sector, where the distance between the story and the substance is widest, and where a collector able to read a movement directly holds the greatest advantage.
[contact-form-7 id=”4235″ title=”Contact form 1″]